

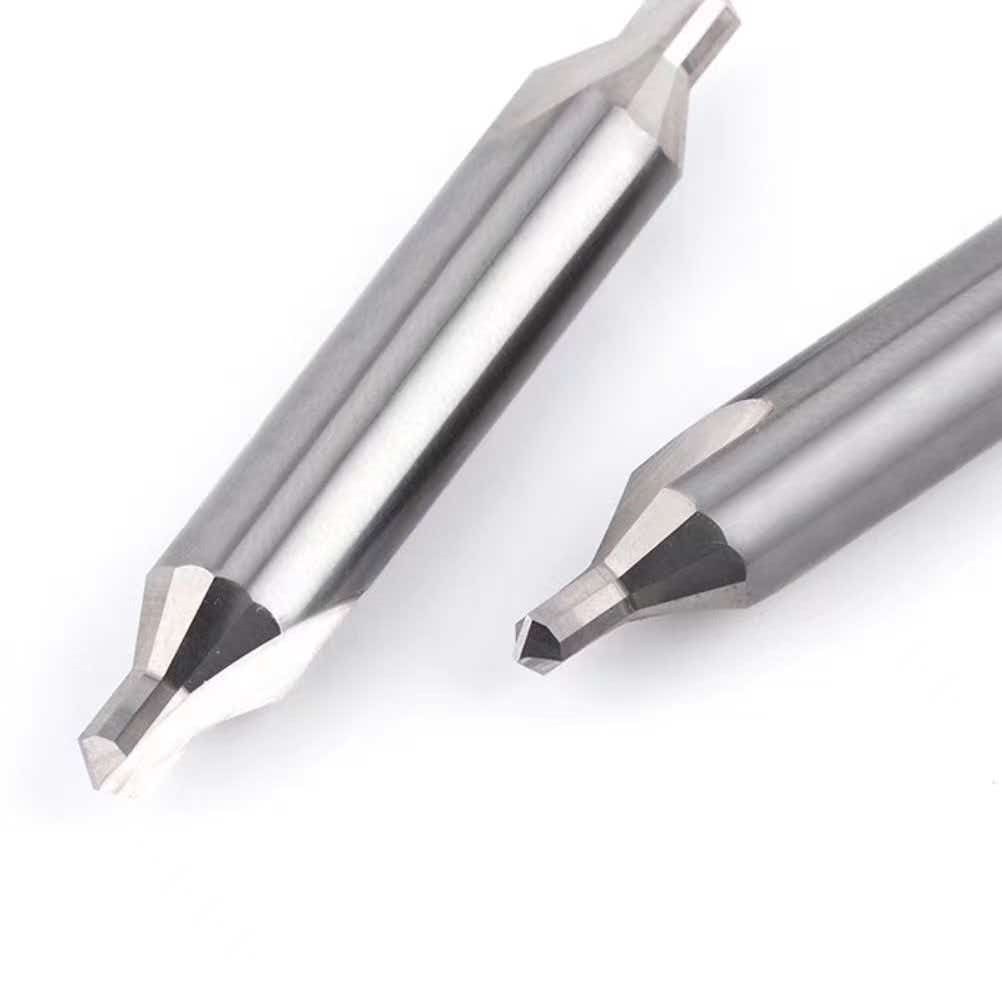
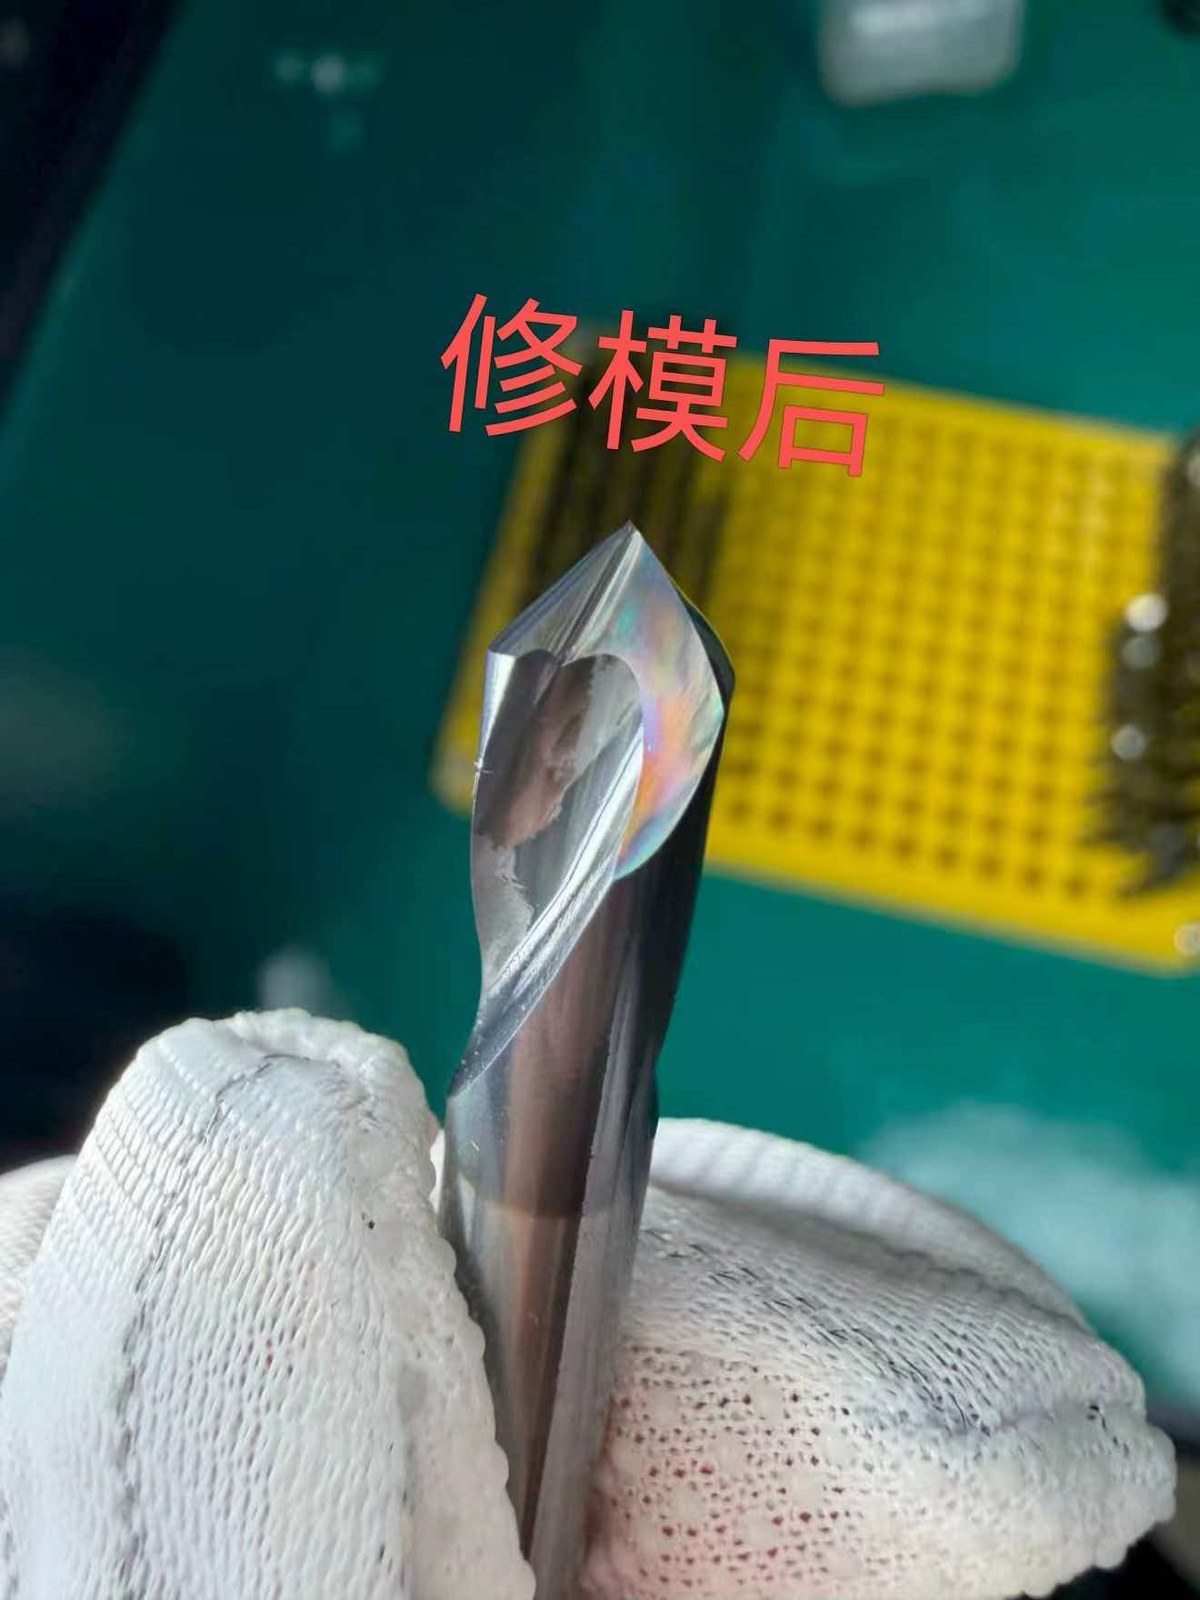
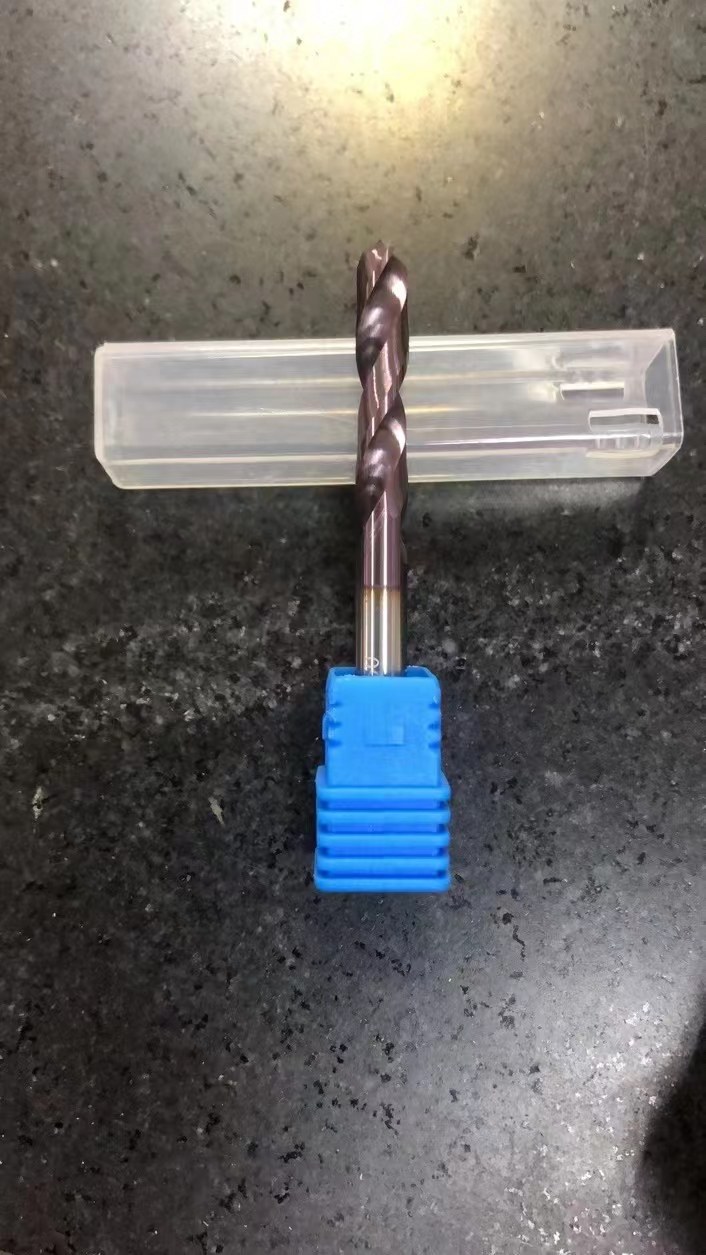
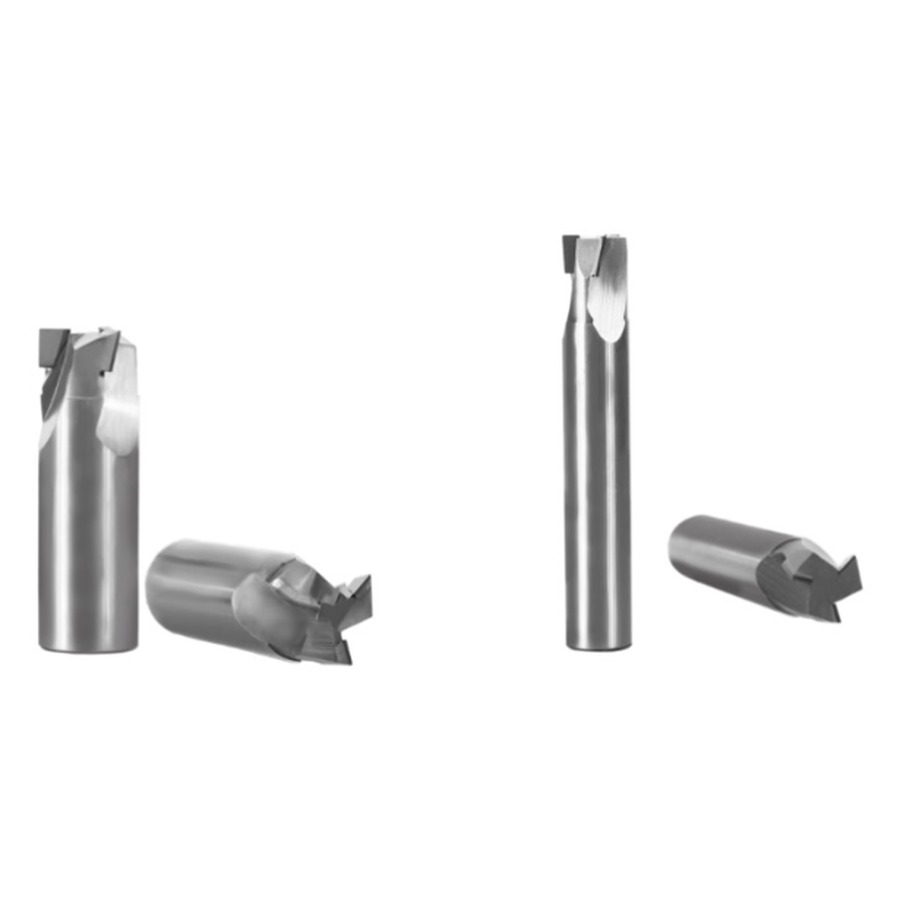
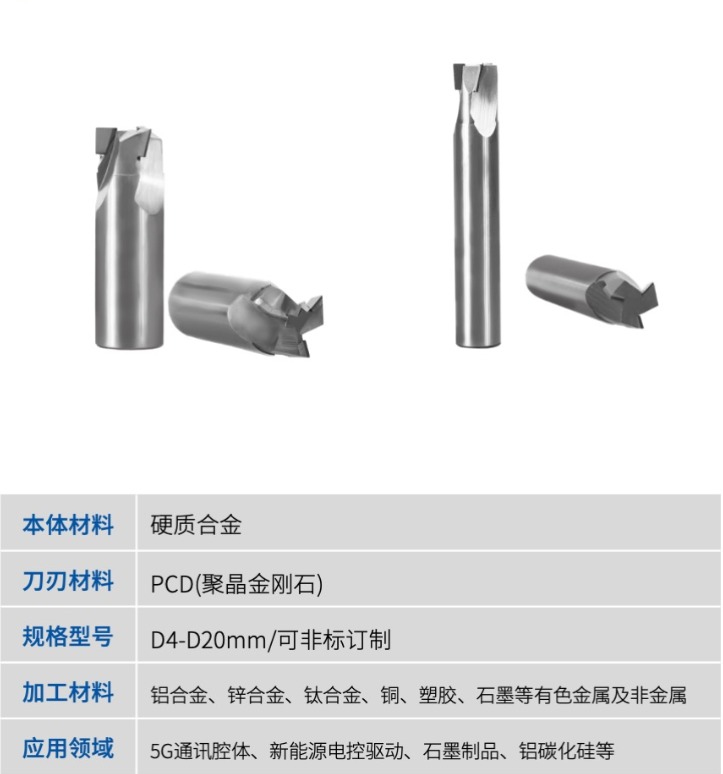
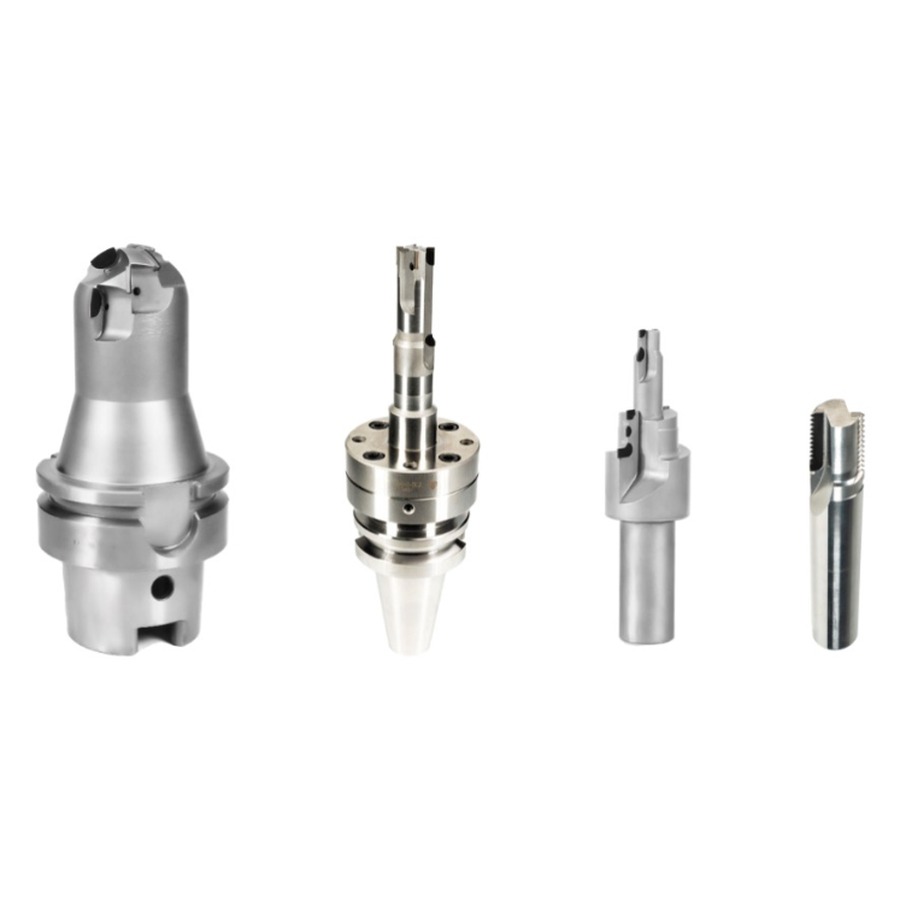
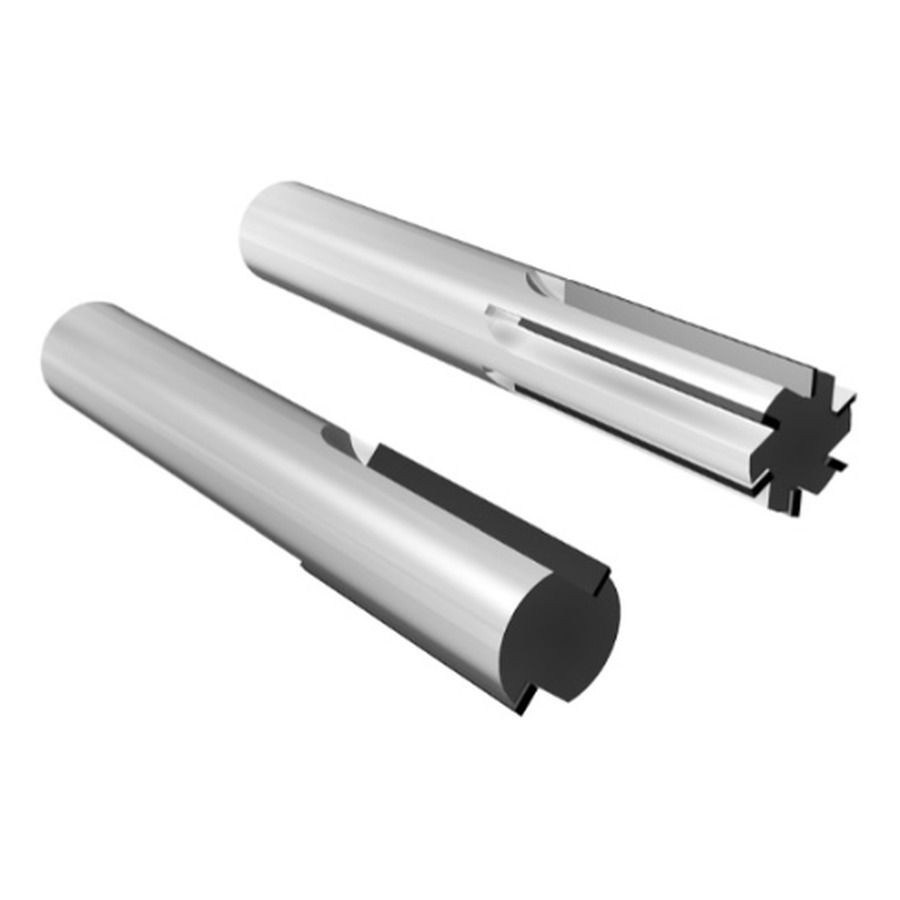
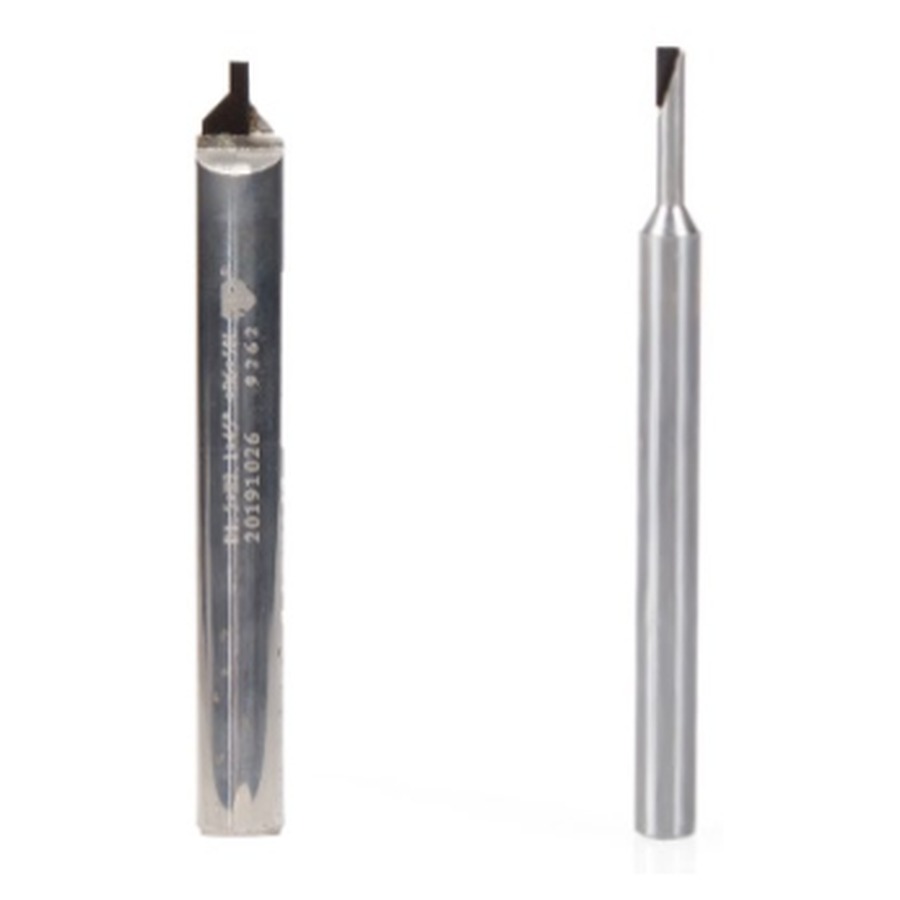
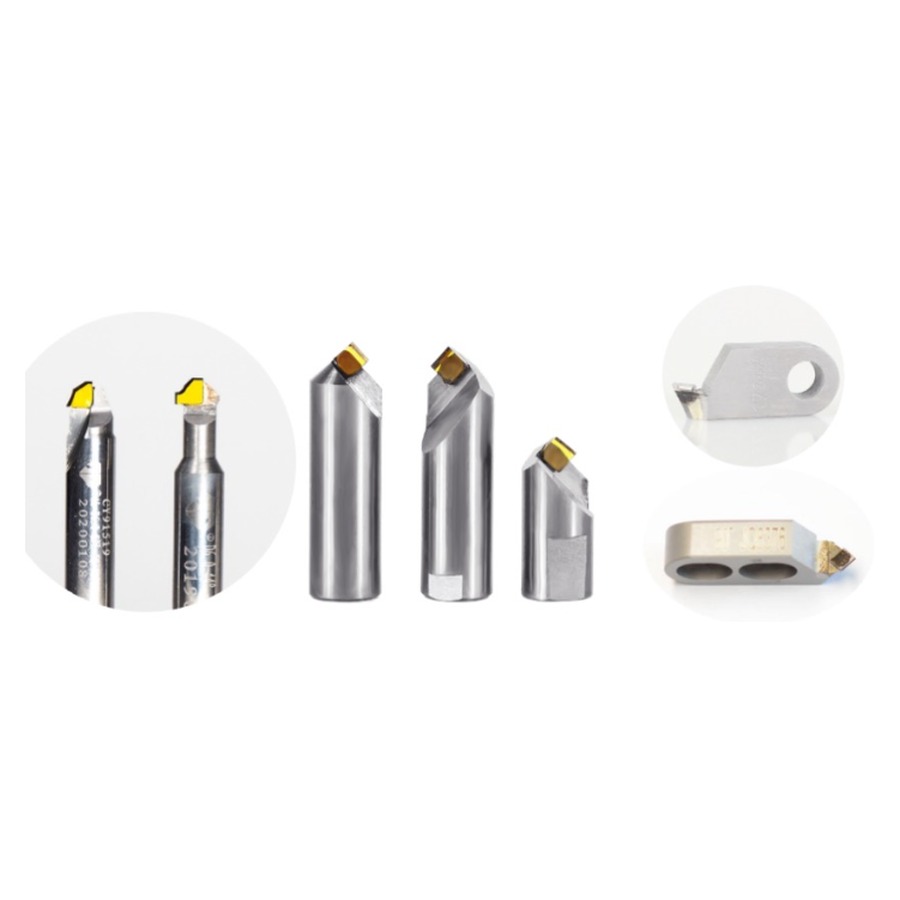
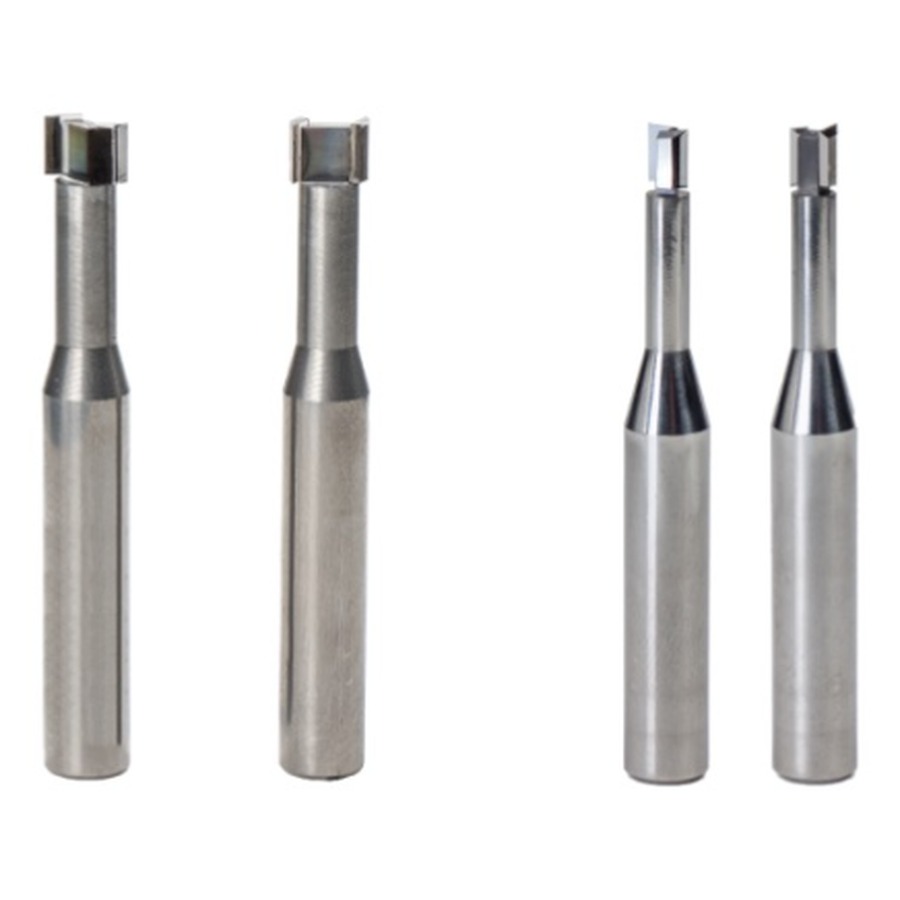
PCD Polycrystalline Diamond End Mill D4-D20mm Full Size Range High Wear Resistance Non Ferrous Machining
GINA PCD刀具专门店

Brands we carry: ZYDK, HZKO, GST, Shibang, Zhengheyuan, Anwei, Mitsubishi, Kyocera, Sumitomo and other Japanese & Korean brands, as well as Seco, Walter, Iscar, Vargus, CPT and more.
-

William Heinrich
19-08-2026Worked with carbide for years on aluminum and decided to bite the bullet on PCD. Worth every cent. Cutting 7075-T6 aerospace bracket, dry, 18,000 RPM, 120 IPM feed, finished in two passes from rough stock to plus-minus 0.02 mm dimensional tolerance. No BUE, no chip weld. Insert swaps are quick and the seat is repeatable within 0.005 mm runout. Quality from this seller is consistent — the third batch from them has been as good as the first.
-
Lucia Fernandez
09-05-2026Honestly, PCD endmills at this price point are a gamble — either they are diamond-plated or properly sintered. These look and cut like properly sintered. We did SEM spot-check and confirmed it is true PCD, not just a coating. Cutting 380 mm cubed per sec MRR on 7075-T6 with no edge build-up. Took 800 parts in our high-silicon die-cast trial before we even saw a hint of wear — that is 4x our previous tool. Highly recommended.
-
Niels van Buuren
15-07-2026Just pulled these out of the box and immediately noticed the diamond edge finish — clean, no chipping. We run 380+ pieces a week of 6061-T6 heatsink plates and these replaced our previous Mitsubishi MET-series. Tool life jumped from ~120 pcs/corner to north of 280 pcs/corner at 14,000 RPM, 0.003 IPT, 0.5 mm DOC. Surface finish on the floor is right at Ra 0.4 without a secondary finish pass. Came in a foam-lined case with an inspection sheet — proper packaging for once. 5 stars, will buy again.
-
Raj Patel
12-04-2026We are an aerospace Tier-2 shop and the lead time quoted was 7 days, actual delivery was 9 days including a weekend. Tool came sharpened, balanced, and individually serialized. Runout measured at 0.003 mm on the test indicator — that's better than the spec sheet claimed. Cutting Ti-6Al-4V? No, this is for our aluminum work, but we did test on a 6061-T6 rib and got plus-minus 0.01 mm on the first part. Will be specifying these on our next RFQ.
-
Jeff Branson
18-06-2026Bought for our optical bracket production line (medical device housings). The roughness we needed was Ra 0.2 on the floor and we could not hit it consistently with our old tungsten carbide. Switched these PCD tools in, dialed back to 16,000 RPM, 80 IPM feed, dry cut, and we got Ra 0.18 right out of the machine. No secondary finishing required. Saved us an entire polishing step. Communication was excellent too — engineer answered my email about speeds and feeds within 4 hours.
Related products
Contact Info
- Address: China
- Email: service@exactalloy.com