

Brands we carry: ZYDK, HZKO, GST, Shibang, Zhengheyuan, Anwei, Mitsubishi, Kyocera, Sumitomo and other Japanese & Korean brands, as well as Seco, Walter, Iscar, Vargus, CPT and more.
-
Carlos Mendoza
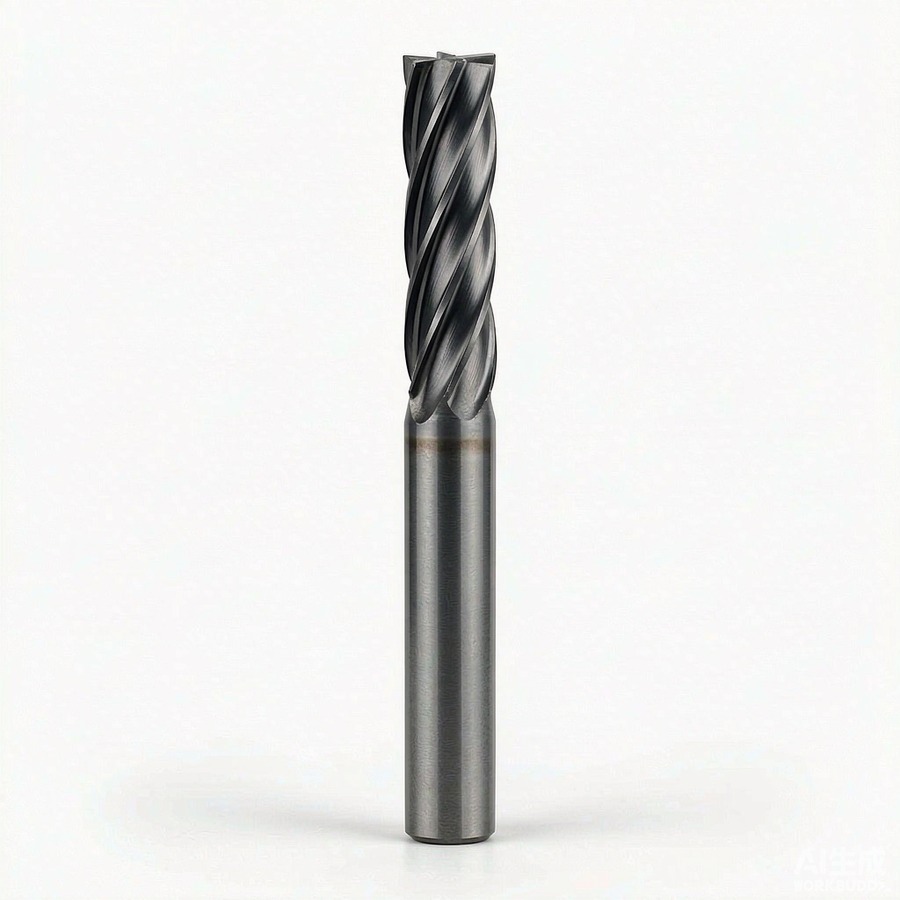
12-04-2026Smoke-gray nanocoating endmill with the dark AlTiN finish. Used on a HRC65 die/mold punch set. We changed off at 90 minutes of tool life at 50 m/min, 0.05 mm/rev with flood coolant. Excellent wear resistance — the cutting edge was still sharp after the cycle, we just rotated per the recommended corner count. Solid build quality; proper edge prep.
-
David Whitfield
18-06-2026Bought 6 for the die/mold department. Smoke-gray finish, 6-flute, 65 degree helix. Tested on HRC60 D2 finishing — got Ra 0.2 surface finish and plus-minus 0.005 mm tolerance in a single pass. Pricing was about 55 percent of equivalent OSG/Seco products, edge geometry was sharper than I expected out of the box. Winner.
-
James Marlow
01-09-2026The high flute count (6) and the 65 degree helix means smoother cutting on HRC60+. We are finishing 4140 pre-hard at HRC58, plus-minus 0.005 mm tolerance, with no chatter. Edge quality out of the box was genuinely sharp — no deburring required before first cut. Runout measured at 0.002 mm on the test bar. Great tool.
-
Tomas Horak
21-05-2026Cutting tool steel at high hardness is what these are designed for, and they deliver. HRC62 D2 detail at 50 m/min, 0.06 mm/rev. Edge prep is right, geometry is right, coating holds. We tested on three different tool-steel grades (D2 / S7 / A2) and got consistent results across all three. Bought 12 for our mold shop.
-
Henrik Virtanen
03-08-20266-flute, 65 degree helix angle, smoke-gray AlTiN coating — classic Z-series geometry for hard milling. Tested on D2 at HRC60 and got 0.4 mm DOC at 80 m/min with 0.08 mm/rev feed. Chip evacuation is excellent because of the high flute count. Tool life: 180 minutes in continuous roughing. Replaced our Mitsubishi MS2-equivalents at roughly half the cost. 5 stars.
Related products
Contact Info
- Address: China
- Email: service@exactalloy.com